Industry
Heavy & Construction Equipment
Parts that carry load through mud, shock and a service interval nobody respects.

FabVector machines Heavy & Construction Equipment parts in Alloy Steel 4140, Carbon Steel 1045, Low-Carbon Steel 1018, from 1 piece, with instant online estimates, engineer-reviewed quotes in 24 hours and NDA-protected files. Delivery with duties handled to the US, Canada, UK and Australia.
- Materials
- Alloy Steel 4140, Carbon Steel 1045, Low-Carbon Steel 1018
- Minimum order
- 1 piece
- Estimate
- ~60s online
- Quote
- engineer-reviewed 24h
- IP
- NDA from upload
What slows this industry down
Heavy machinery parts fail at the interfaces, not in the middle. A pivot pin that is two hundredths oversize seizes in the bushing after the first wet season; one that is undersize hammers the bore oval within a thousand hours. That makes the fit class, the surface finish in the bearing area and the hardness after treatment the whole job — the outside profile is almost decoration. Aftermarket and retrofit orders arrive without drawings, as a worn sample and a request to "make it like this but better", which needs someone willing to measure and produce a print before quoting. And the parts are heavy and awkward: a 40 kg housing costs more to ship wrong than it did to cut, so first-article approval before batch release is not bureaucracy, it is freight insurance.
Typical parts we machine
- Hydraulic cylinder end caps and gland nuts
- Pivot pins, bushings and thrust washers
- Gearbox and final-drive housings
- Boom, arm and linkage brackets
- Valve blocks and port manifolds
Recommended materials
Alloy Steel 4140
Chromoly muscle: deep-hardening alloy steel for heavily loaded shafts, tooling and gears.
Carbon Steel 1045
The shaft steel: strong, cheap, induction-hardenable exactly where it counts.
Low-Carbon Steel 1018
The friendly mild steel: welds beautifully, case-hardens to a glassy skin, costs less than anything.
Aluminum 6061-T6
The default CNC aluminum: strong enough for most jobs, machines fast, anodizes well.
Phosphor Bronze C510
The spring bronze: fatigue resistance and low-friction wear for contacts and bushings.
Recommended finishes
Black Oxide
Black with zero dimensional change: the gauge-and-tool finish for precision steel.
Zinc Plating
The economy rust-stopper: sacrificial zinc keeps protecting even when scratched.
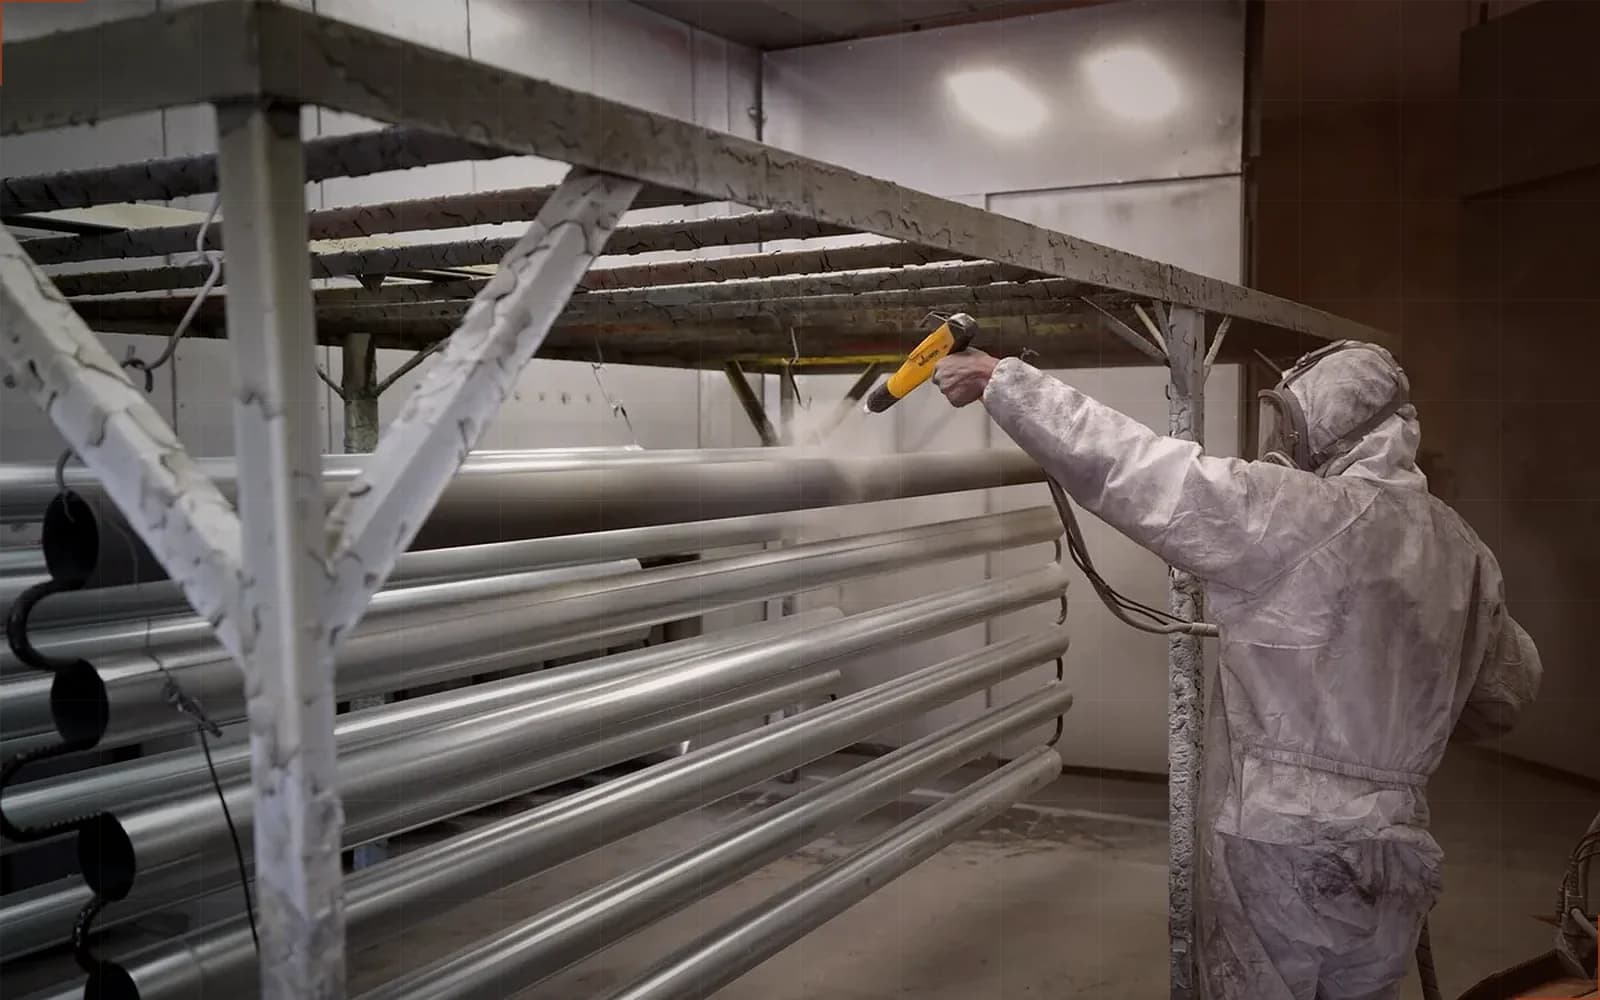
Powder Coating
Baked-on polymer armor: any RAL color, outdoor-proof, the toughest cosmetic coating.
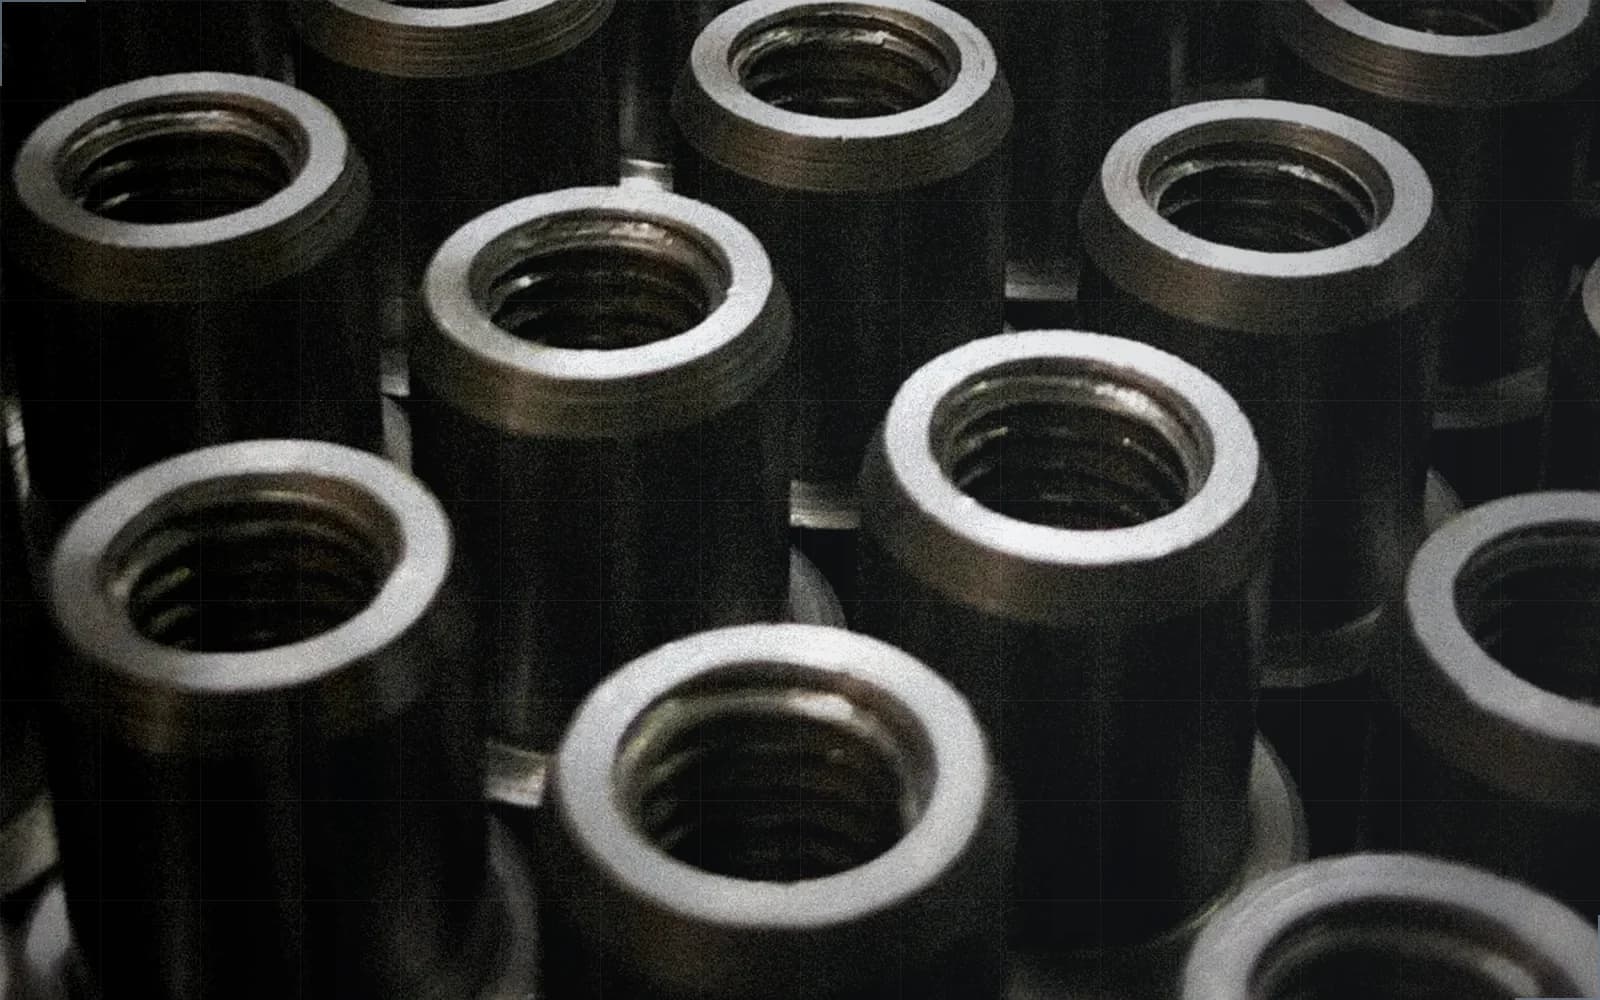
Hard Chrome Plating
The hardest plated surface in the shop: ~65 HRC chrome for sliding and abrasive service.
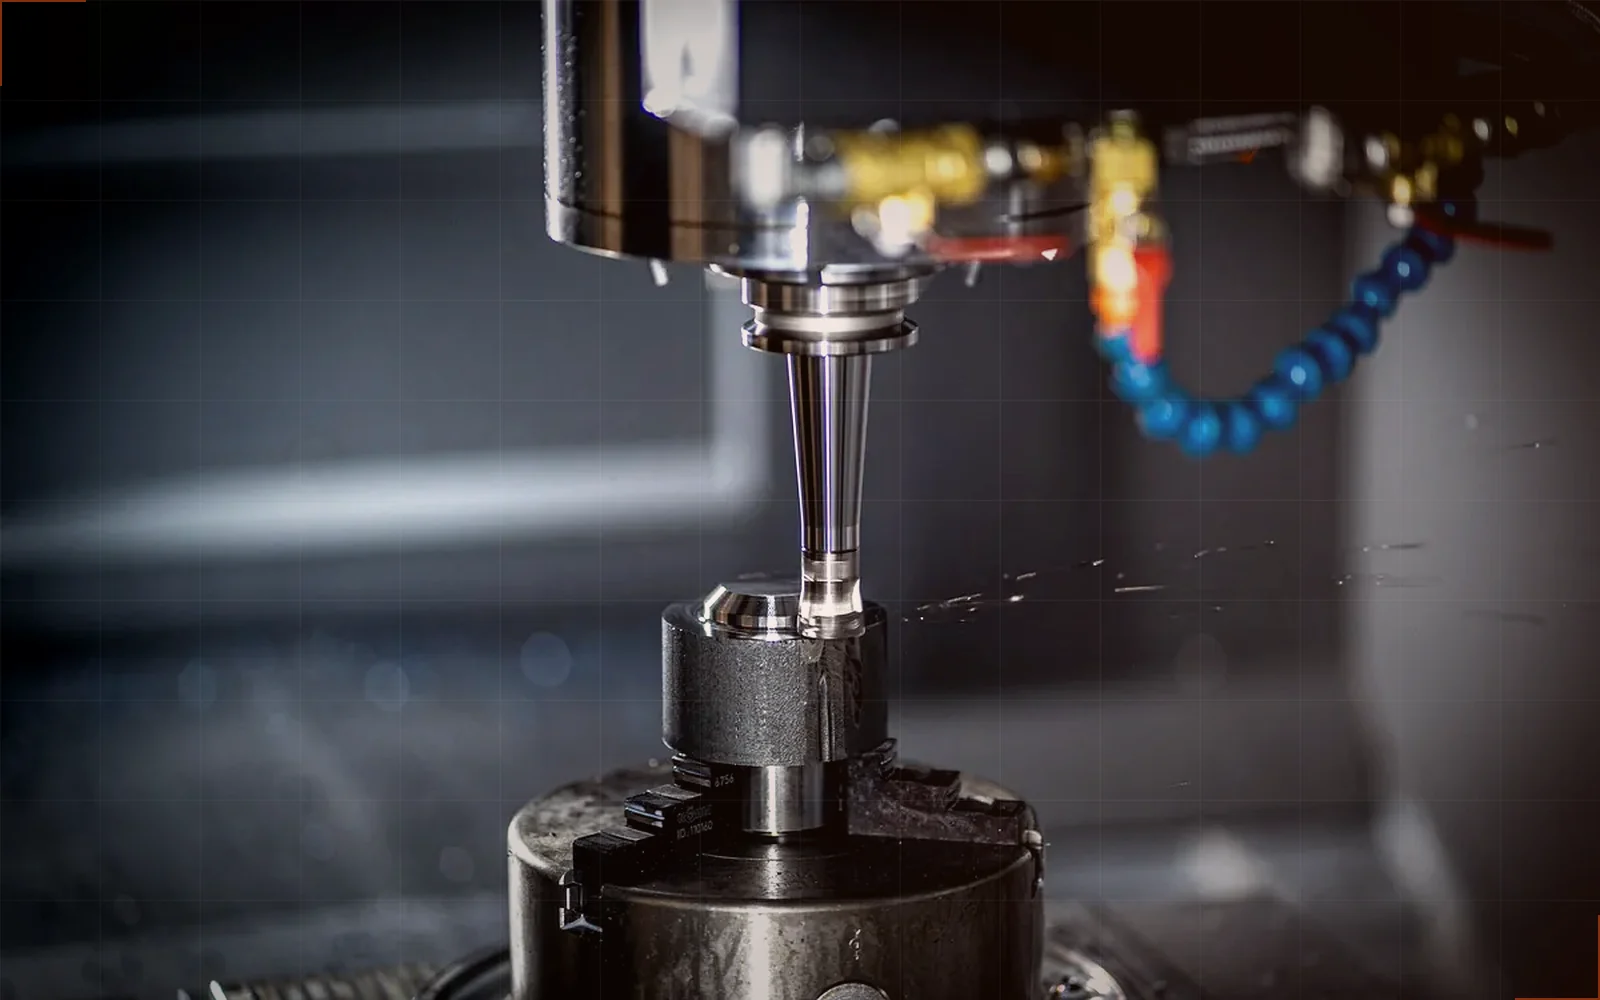
As-Machined
The baseline finish: straight off the machine, fastest and cheapest.
Certifications & standards
- ISO 9001
- We understand equipment OEMs expect ISO 9001-grade control on fit-critical features, with the bearing diameters and bore fits recorded rather than spot-checked.
- EN 10204 3.1
- We support EN 10204 3.1 certificates on 4140 and 1045 load-path parts, where the delivered mechanical properties are what the structural calculation assumed.
- ISO 2768-m / ISO 286
- General tolerances plus an explicit fit class on pins and bores; we quote against the fit, not the nominal diameter, because that is the dimension that decides service life.
We understand and support these requirements; certification and documentation scope is confirmed per order.
Questions heavy & construction equipment buyers ask
- Can FabVector supply forged and machined heavy-equipment parts under one order?
- Yes, by engineering-reviewed RFQ. FabVector can coordinate the forged blank, heat treatment, CNC finish machining, coating and dimensional inspection for pins, links, yokes, shafts and other load-path parts. Send finished CAD, material, annual volume and load direction so forging route, tooling, grain flow and machining allowance are reviewed together.
- What fit class should pivot pins and bushings be machined to?
- Specify the fit, not just diameters — typically H8/f7 running fits for greased pivots, tighter where side load fights slop. A pin two hundredths oversize seizes after the first wet season; undersize hammers the bore oval within a thousand hours. We inspect pins and bores as mating pairs when both are on the order.
- Can a worn part be reverse-engineered without a drawing?
- Yes — aftermarket and retrofit work often arrives as a worn sample and "make it like this but better". We measure, reconstruct nominal dimensions accounting for wear, produce a print for your approval, then machine to it. The print approval step is not optional: it is where "better" gets defined in numbers.
- Why insist on first-article approval before releasing a batch of heavy parts?
- Because a 40 kg housing costs more to ship back wrong than it cost to machine. FAI before batch release converts freight risk into one part's worth of schedule — on international heavy work that trade is arithmetic, not caution.
Relevant services
CNC Turning
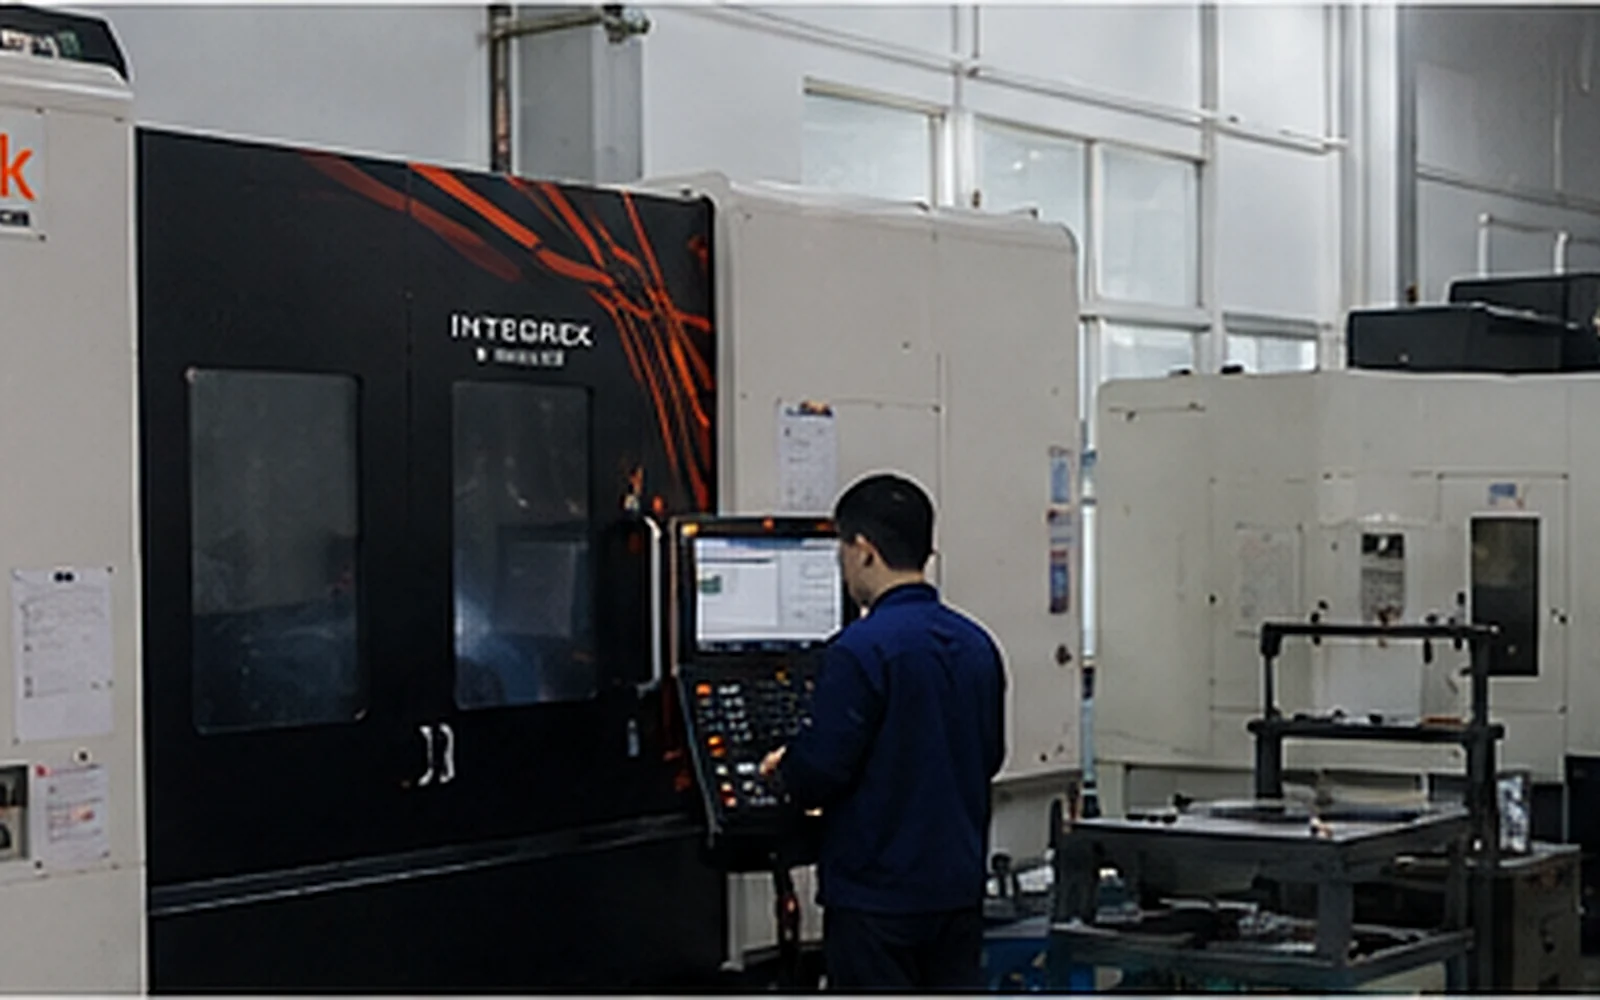
Live-tooling lathes for shafts, pins, bushings and threaded fittings up to Ø406 mm.
CNC Milling
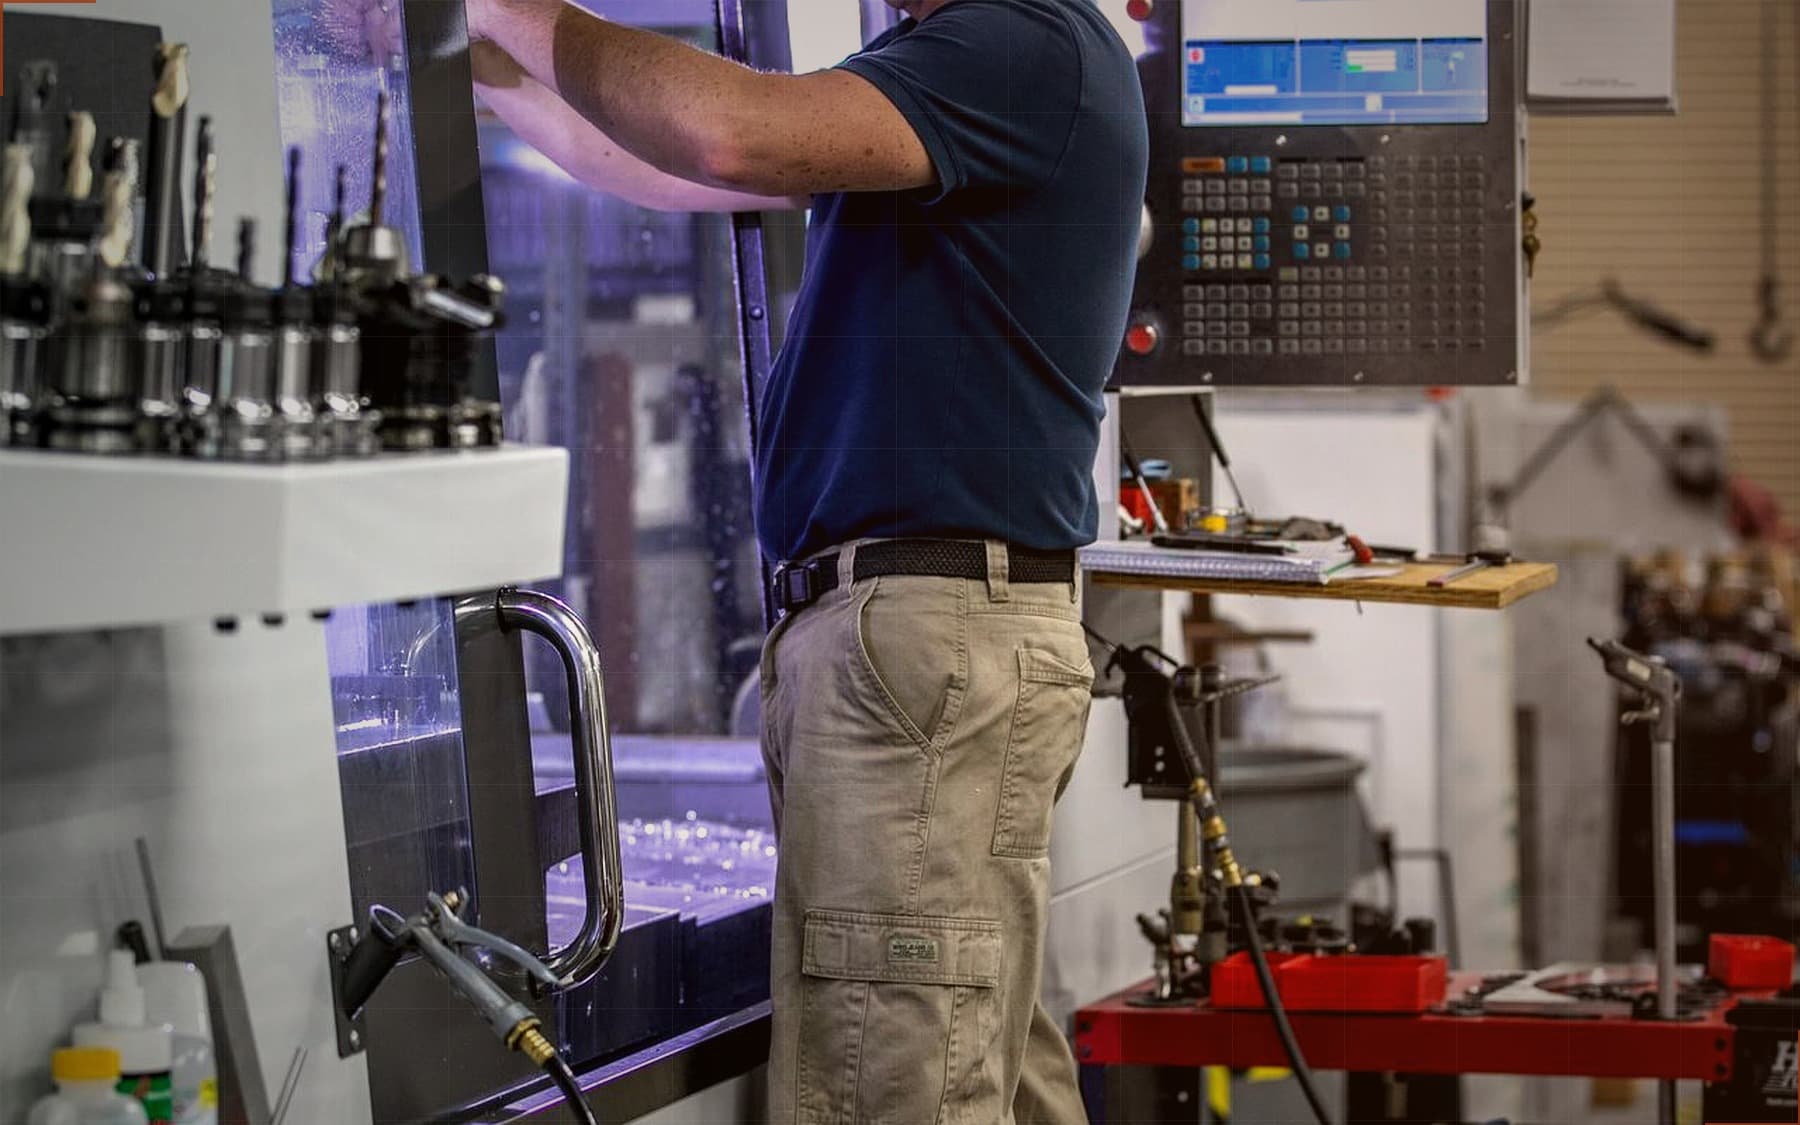
3- and 4-axis vertical machining for housings, brackets, manifolds and structural parts.
Production Machining
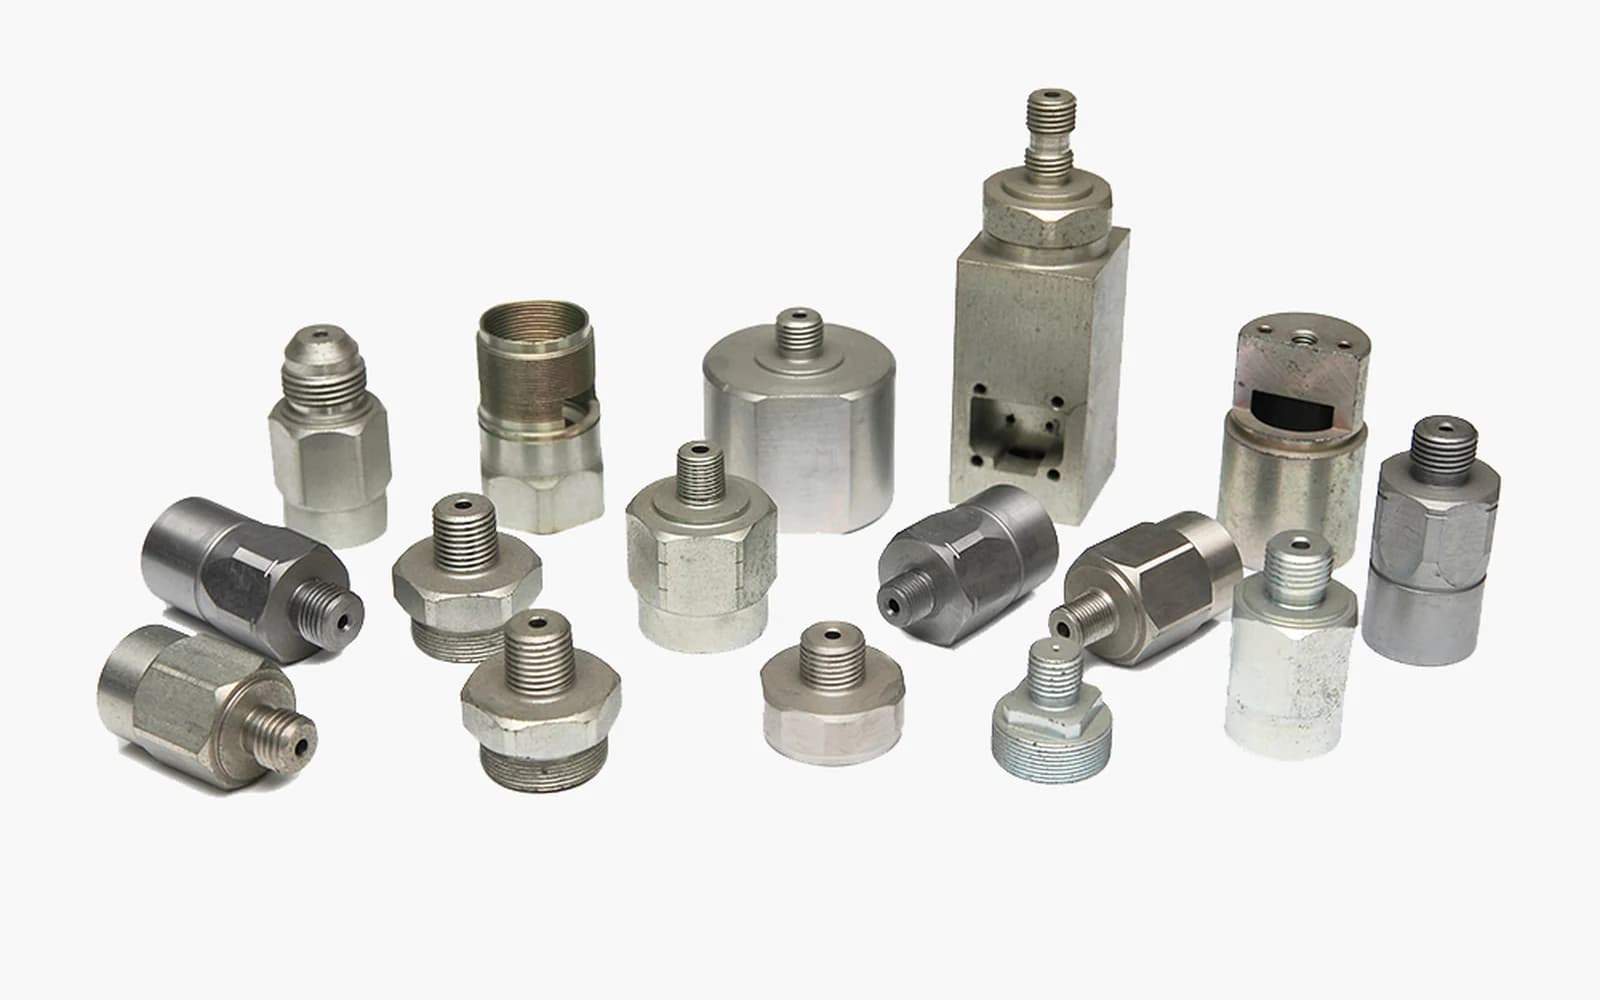
Dedicated fixturing, in-process CMM and SPC documentation for repeatable volume runs.
Surface Grinding
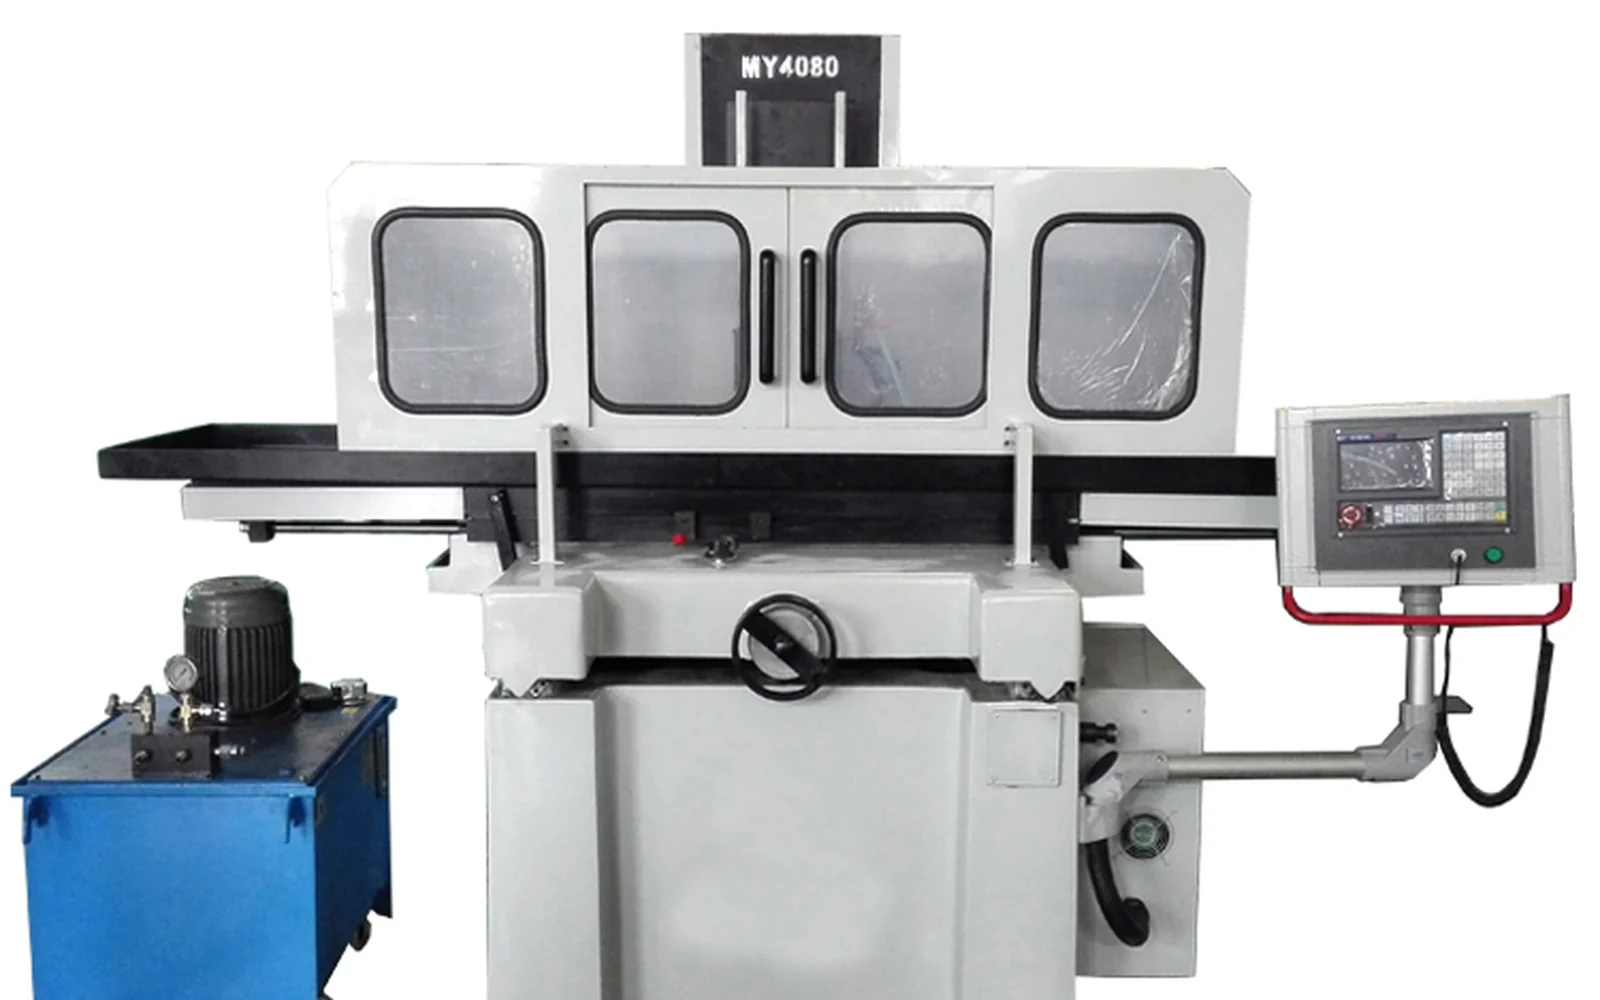
Abrasive finishing for flatness, parallelism and tight thickness control on hardened parts.
Custom Forging
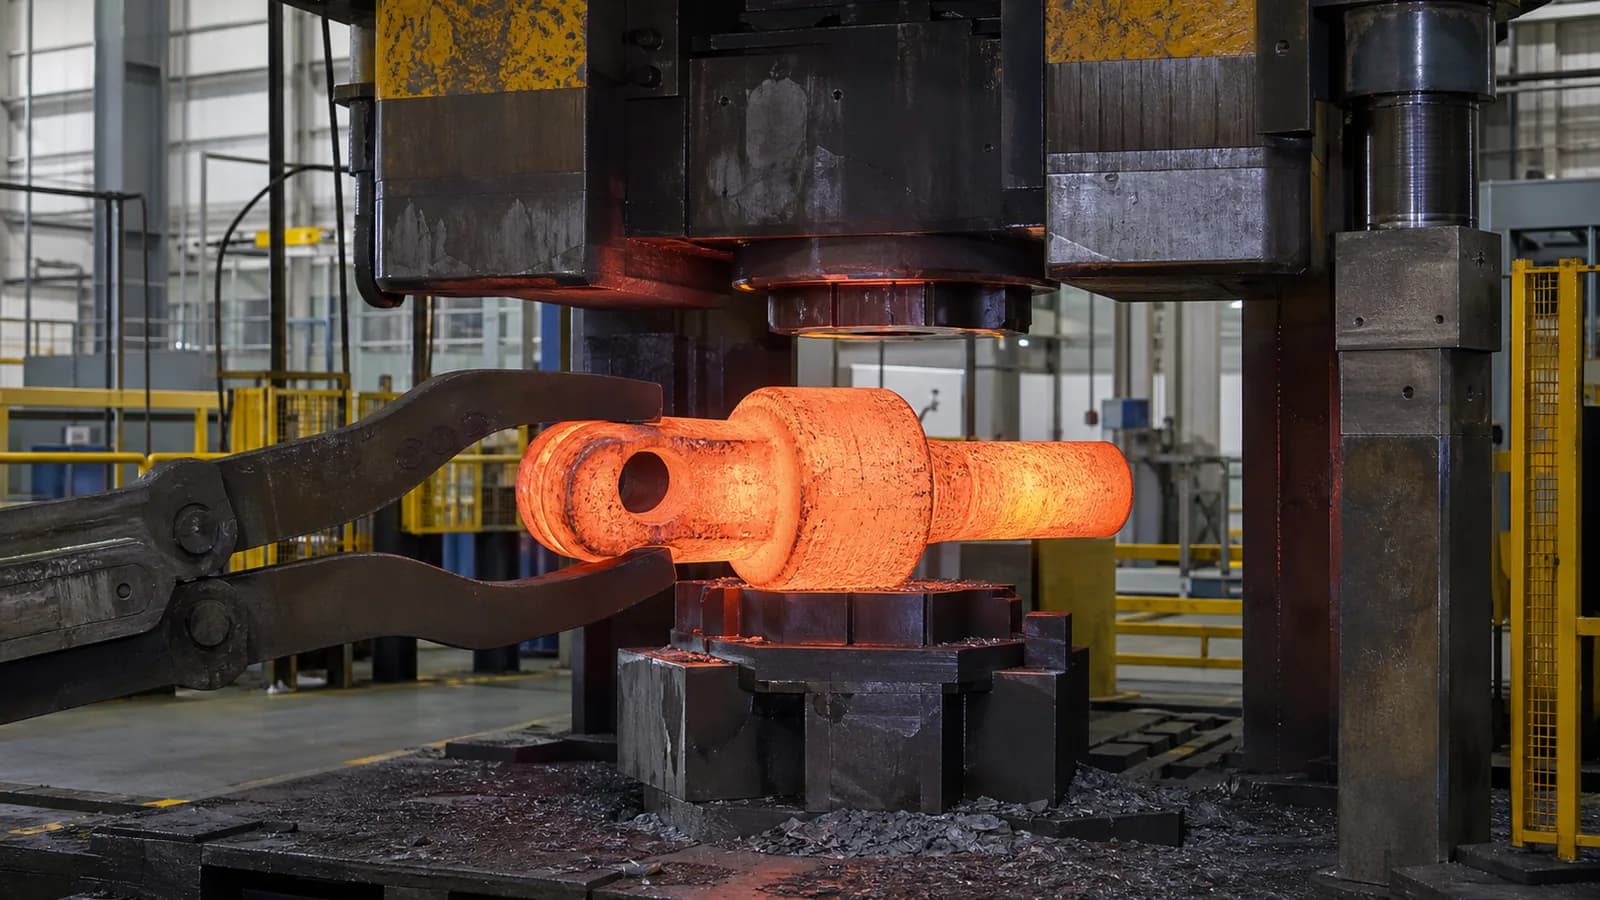
Forged blanks and finished load-bearing parts, with tooling, machining, heat treatment and inspection coordinated as one program.
CNC machining service by country
Replacement and spares programmes are transfers by another name. Work through the transfer checklist before you send a legacy drawing out for quote.
Have a part in mind?
Upload CAD or drawings. Eligible CNC work gets an instant estimate; other processes move to engineer review. NDA-protected from the first byte.
Start an RFQ